Language
When operating a laser cutting machine, excessive burrs and heavy dross on the cut surface are the primary causes of workpiece rejection. While many operators instinctively try replacing lenses or adjusting power, the true determinants of cut quality often lie in frequently overlooked process parameters and nozzle details. To resolve issues with burrs and dross, one must precisely address parameter matching and nozzle management.
1. Focus parameters act as the "master switch" for controlling dross. A deviation of just 0.5 mm in the focal position causes drastic fluctuations in the laser's energy density. If the focus is too deep, energy at the bottom of the cut is insufficient, causing molten slag to cool and form hard burrs; if the focus is too shallow, energy remains concentrated at the surface, resulting in thicker dross accumulation at the bottom. For a given machine, the focus should be raised when cutting stainless steel and lowered when cutting carbon steel; adjusting this key parameter can directly reduce dross thickness by 40%.
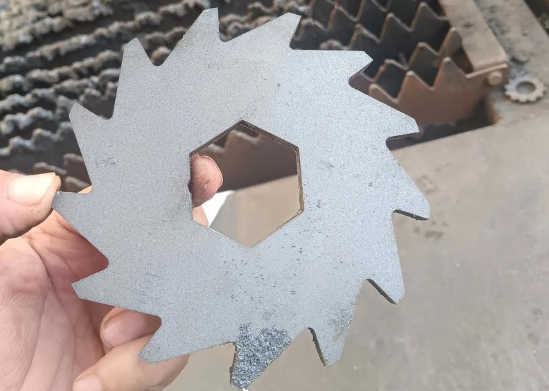
2. Gas parameters serve as the "cleanup crew" for removing dross. Assist gas pressure and purity directly impact the machine's slag-clearing capability. If pressure is too low, molten material isn't fully blown away, causing burrs to adhere firmly; if pressure is too high, turbulent airflow can actually force dross against the edges of the cut. Particular attention must be paid to purity: oxygen purity below 99.5% leads to oxidative dross when cutting carbon steel, while impure nitrogen causes blackening and burrs on stainless steel cut surfaces. When adjusting gas parameters, ensure the airflow exiting the nozzle forms a straight, conical shape—a fundamental requirement for effective dross removal.
3. Nozzle factors are often a "hidden hotspot" for dross issues. If the nozzle aperture does not match the sheet thickness, the gas diffusion area will be either insufficient—leading to dross accumulation at the bottom—or excessive, causing a pressure drop that fails to clear away burrs. More importantly, the cleanliness of the nozzle tip directly determines the coaxiality of the airflow; a single speck of spatter on the nozzle can result in a cut with a smooth side and a burr-filled side—an uneven finish. It is recommended to inspect the nozzle tip during every shift, using fine sandpaper to gently remove adhered slag, and to replace the ceramic ring monthly to ensure the nozzle center deviation remains under 0.05 mm. If these nozzle-related factors are neglected, even a high-power laser cutter will fail to produce a quality cut surface.
Furthermore, the cutting speed must be coordinated with the aforementioned factors: excessive speed leads to trailing burrs, while insufficient speed causes slag adhesion and ablation. Resolving issues like excessive burrs and heavy slag accumulation is never a matter of a single adjustment; rather, it requires systematic optimization involving focus settings, gas parameters, and nozzle conditions. The next time you encounter a rough or unsatisfactory cut surface, first review your parameter settings and then clean the nozzle tip; once this "golden combination" is properly set, the cut surface will naturally become smooth and mirror-like. Remember: manage your parameters and nozzle, and you effectively manage the quality of your laser cutting.
Copyright © 2008-2022 Morn Laser All Rights Reserved.