Language
When your laser cutting machine produces parts with rough, striated edges instead of clean, smooth cuts, it signals underlying issues that need immediate attention. Poor edge quality not only affects aesthetic appearance but also compromises weldability and subsequent machining operations. This guide provides a systematic approach to diagnosing and resolving edge roughness problems.
Assist gas plays a critical role in expelling molten material from the kerf. If gas pressure is too low, slag accumulates along the cut edge, creating roughness. If pressure is too high, turbulent flow causes secondary burning and uneven surfaces.
Fix: Verify that your laser cutting machine's assist gas pressure matches the recommended settings for the material type and thickness. For mild steel, oxygen pressure should typically range between 0.6-1.0 MPa. Also, check gas purity — oxygen below 99.5% or nitrogen below 99.9% can significantly degrade cut quality. Replace gas filters if contamination is suspected.
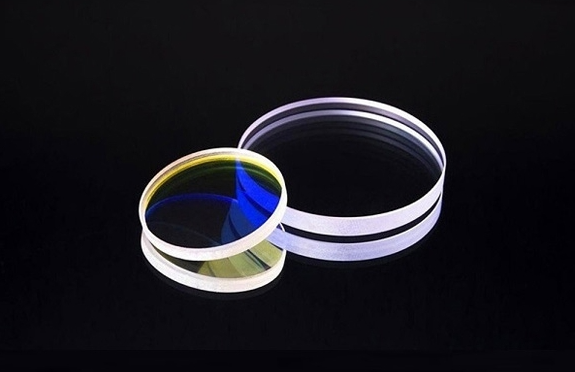
Contaminated optics scatter the laser beam, creating an irregular energy distribution at the focal point. This produces inconsistent melting and rough edges. The protective lens is most vulnerable to spatter and dust.
Fix: Remove the protective lens from your laser cutting machine and inspect under bright light. Use optical-grade cleaning solution and lint-free wipes to clean from center outward. Also check the focusing lens and collimating lens inside the optical cavity. Clean all optics following proper procedures. Even minor contamination can cause noticeable roughness.
Incorrect focal position is one of the most common causes of poor edge quality. If the focus point is too high or too low relative to the material surface, the beam loses cutting efficiency and creates rough kerfs.
Fix: Run a focal position test on your laser cutting machine. Cut a series of lines on scrap material with incremental focus offsets, then examine cross-sections to identify the optimal focus position. This "focus finder" test helps determine the exact setting for cleanest edges.
A worn or misaligned nozzle disrupts gas flow dynamics, leading to uneven removal of molten material. This is particularly noticeable when cutting thicker materials.
Fix: Inspect the nozzle orifice — if it appears ovalized or has burn marks, replace it. Then check nozzle centering. On your laser cutting machine, perform a nozzle alignment test by firing a low-power pulse through thermal paper placed under the nozzle. The burn mark should be perfectly centered. Adjust the centering screws if necessary.
Excessive cutting speed reduces residence time, preventing complete material melting and expulsion. Conversely, too slow a speed creates a wide heat-affected zone and increased dross formation.
Fix: Consult your laser cutting machine's parameter table for recommended speed and power settings. If roughness persists, try reducing speed by 10-15% and adjusting power accordingly. Keep a log of successful parameters for each material-thickness combination — this becomes a valuable reference as conditions change.
| Issue | Checkpoint | Resolution |
|---|---|---|
| Rough edge with slag | Gas pressure low | Increase pressure or replace gas |
| Uneven roughness | Optics contaminated | Clean protective/focusing lenses |
| Consistent roughness | Focal position off | Perform focus test and adjust |
| One-sided roughness | Nozzle misaligned | Center the nozzle |
| All cuts rough | Parameter mismatch | Adjust speed/power settings |
Daily: Clean the protective lens and check nozzle condition
Weekly: Verify gas pressure readings against baseline records
Monthly: Perform a full optical path inspection
Per Material Batch: Run a test cut before production runs
A well-maintained laser cutting machine consistently delivers clean, smooth edges. By following this systematic troubleshooting process, you can identify the root cause of roughness and restore cut quality quickly. If issues persist after all checks, consult your equipment manufacturer's technical support team.
Copyright © 2008-2022 Morn Laser All Rights Reserved.